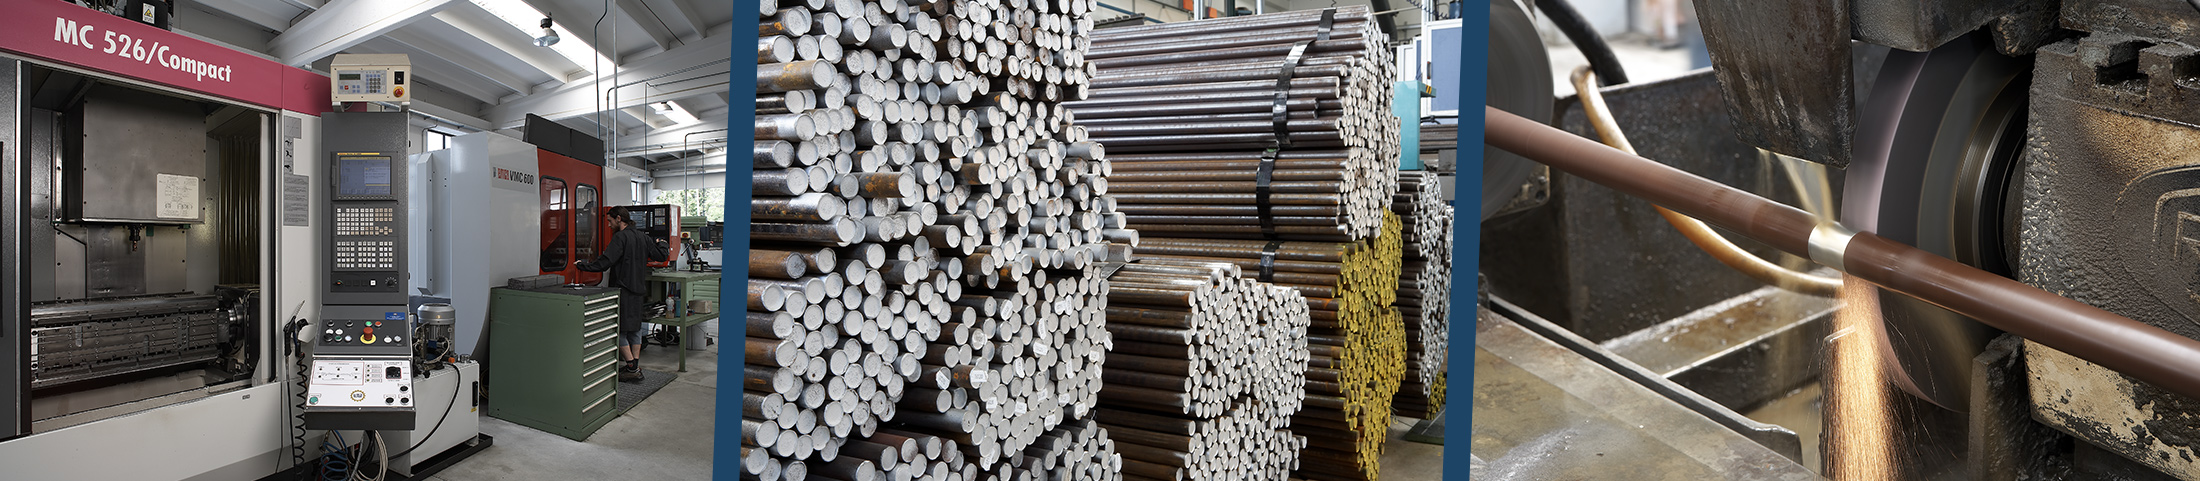
The production cycle begins with raw steel bars acquired under strict, precise specifications, which are immediately cut and deep-hole drilled to size. Next, initial internal operations are carried out, including reaming and chambering.
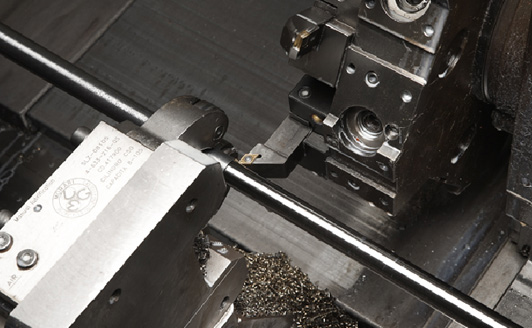
Following an initial dimensional inspection, the external profile is machined: turning, threading, external lapping, and washing—all followed by a second inspection using dedicated measurement tools. Concurrently, top and side ribs are manufactured.
All components are then manually assembled by specialized technicians using fixtures specifically designed and engineered for this operation.
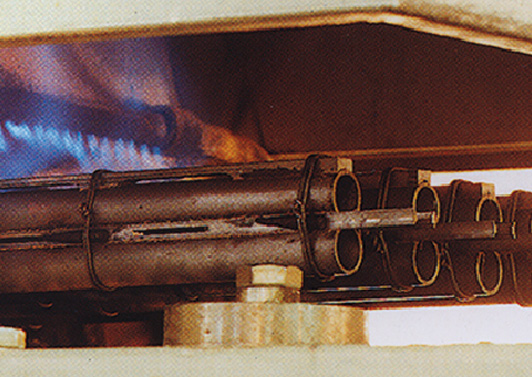
Silver brazing—a crucial and delicate stage in barrel assembly—is performed in a controlled atmosphere furnace using a silver-based alloy at a temperature of approximately 700°C.
Excess brazing alloy is subsequently removed through an electrolysis process, taking special care to maintain the structural integrity of the joint. This step is completed in a computerized, closed-loop system in full compliance with environmental regulations.
The subsequent internal lapping process delivers a high surface finish. Our system enables precise finishing in critical barrel zones where traditional lapping is less effective, such as the chamber, forcing cones, and choke section.
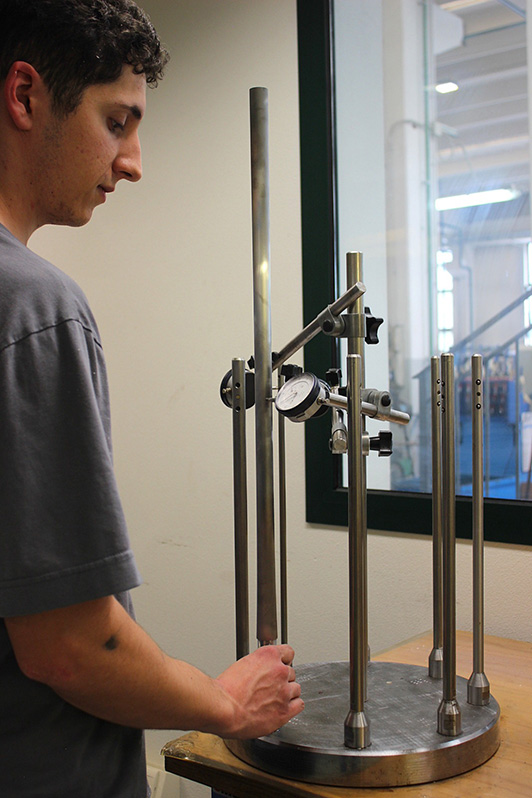
The final phase is a rigorous quality control check, relying on extensive expertise to ensure that every barrel is defect-free and compliant with our standards.
Do you have any questions or would you like to receive more information about our products?
Our dedicated staff will be happy to assist you and provide custom technical consulting tailored to your needs!
Contact us via email at info@bfim.it
or call us at 030.850016.
Localita' Prade 2/a - 25060 Lodrino (Brescia)